Aluminum Materials Used in Rail Transportation
1, Introduction
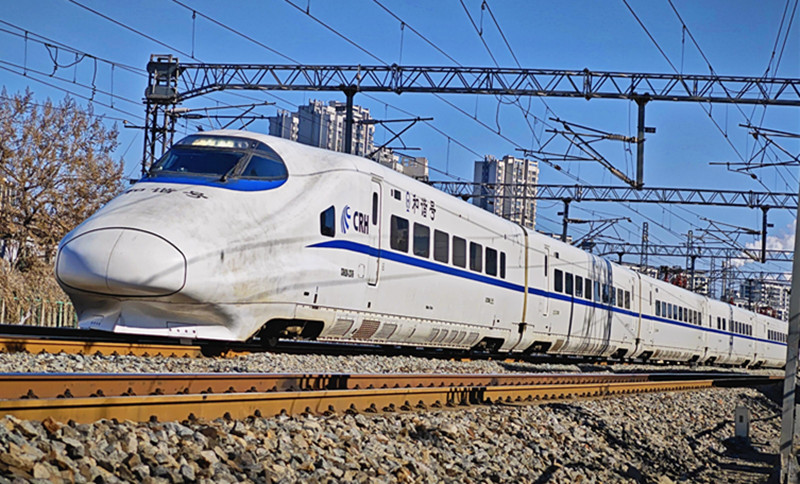
Aluminum alloys are widely used in modern rail transportation vehicles because of their low density, corrosion resistance, and processing flexibility. Reducing vehicle weight helps lower energy consumption and improve operational efficiency, making aluminum alloys important materials in the manufacturing of high-speed trains, conventional trains, and metro vehicles.
In rail vehicles, aluminum alloys are primarily used in carbody structures and interior components. Cast aluminum alloys are also used to manufacture components such as gearbox housings. Different applications require different material forms, alloy grades, and processing methods. Large hollow extrusions are particularly important in carbody construction, while aluminum sheets are commonly used for interior panels and cast aluminum alloys are suitable for complex gearbox housing structures.
2. Aluminum Alloys for Train Carbody Structures
The carbody is one of the most important applications of aluminum alloys in rail transportation. Aluminum alloy carbody structures help reduce vehicle weight while providing the strength and structural integrity required for operation.
2.1 6005A and 6082 Aluminum Alloys
6005A aluminum alloy is widely used in rail vehicle manufacturing, particularly for large hollow extruded profiles used in carbody structures. Its combination of strength, extrudability, and weldability makes it suitable for manufacturing complex structural sections.
6082 aluminum alloy is another 6xxx-series alloy used for selected structural members and components. Depending on the design requirements, aluminum plates, extrusions, and machined parts can be incorporated into different parts of a train structure.
| Aluminum Alloy | Material Form | Typical Applications |
|---|---|---|
| 6005A | Large hollow extruded profiles | Carbody side walls, roof panels, and floor structures |
| 6082 | Extrusions, plates, and machined components | Selected load-bearing structures and structural components |
| 5083 | Aluminum plate | Selected plate-based structures |
2.2 Why Hollow Extrusions Are Used in Carbody Manufacturing
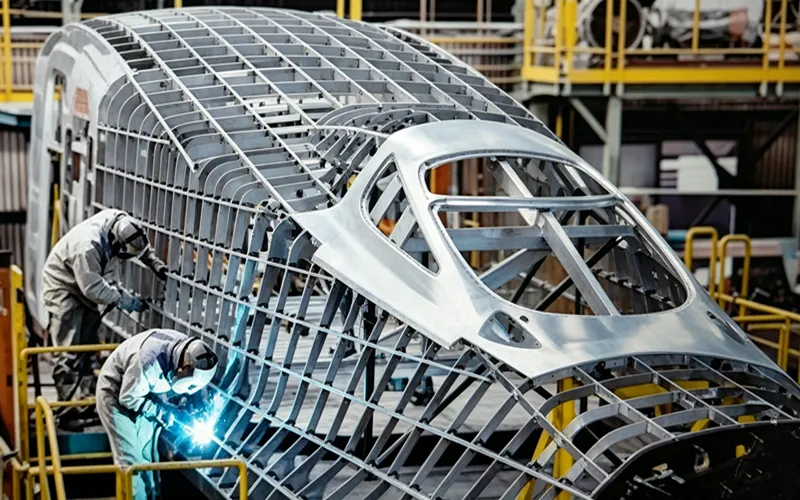
Large hollow extruded profiles are a key feature of aluminum rail vehicle construction. Their cross-sectional geometry can incorporate cavities, reinforcing ribs, and different wall thicknesses into a single profile. This allows designers to combine structural functions while controlling weight.
For example, hollow extrusions can be arranged side by side to form carbody side walls, roof sections, and floor structures. The profile design determines how loads are distributed through the structure, while reinforcing ribs and carefully designed transitions help manage stress concentrations.
The use of large extrusions also reduces the number of individual components required for assembly. This supports a more integrated structural design and helps improve manufacturing efficiency.
2.3 Welding and Structural Reliability
Welding is an important process in the assembly of aluminum carbody structures. Friction stir welding (FSW) is used to join aluminum hollow extrusions and is particularly relevant to rail vehicle manufacturing.
Compared with conventional fusion welding, friction stir welding can reduce welding distortion and help produce consistent joints in aluminum structures. The process has been studied extensively for 6005A-T6 hollow extrusions used in railway vehicles.
Welding conditions and joint geometry affect the mechanical properties of the finished structure. For heat-treatable alloys such as 6005A-T6, the heat-affected region can experience changes in hardness and strength. Joint design, welding parameters, and structural testing therefore play important roles in ensuring the reliability of the completed carbody.
Fatigue performance is also important because train structures experience repeated loading during operation. Profile geometry, weld quality, and stress distribution all contribute to long-term structural performance.
3. Aluminum Alloys for Train Interior Components
Aluminum alloys are also used in train interiors, including interior panels, ceiling panels, door frames, partition frames, and decorative profiles. These components require a combination of formability, surface quality, corrosion resistance, and appropriate fire performance.
3.1 Aluminum Sheets for Interior Panels
3003 and 5052 aluminum alloys are suitable material options for selected interior sheet applications.
3003 aluminum alloy offers good formability and is suitable for components that require bending and forming. It can be used to manufacture interior panels and other formed sheet components.
5052 aluminum alloy provides higher strength than 3003 in many commonly supplied conditions, together with good corrosion resistance. It is suitable for interior components that require a stronger sheet material.
| Aluminum Alloy | Main Characteristics | Typical Applications |
|---|---|---|
| 3003 | Good formability and corrosion resistance | Formed interior panels and sheet components |
| 5052 | Good strength, formability, and corrosion resistance | Interior panels and components requiring greater strength |
| 6xxx-series alloys | Extrudability and structural versatility | Frames, supporting profiles, and door-frame components |
3.2 Forming and Surface Finishing
Interior aluminum components are commonly produced through processes such as cutting, punching, bending, and surface finishing. The selected alloy and temper influence how the material behaves during forming and the quality of the finished component.
Surface treatments and coatings can be applied to meet appearance, cleaning, and service requirements. Consistent surface quality is particularly important for visible interior panels and decorative components.
Fire performance is another important consideration in rail vehicle interiors. Materials and components used in railway vehicles are subject to applicable fire protection requirements, including EN 45545-2. Material selection and the complete component configuration must meet the relevant requirements for the intended application.
4. Cast Aluminum Alloys for Train Gearbox Housings
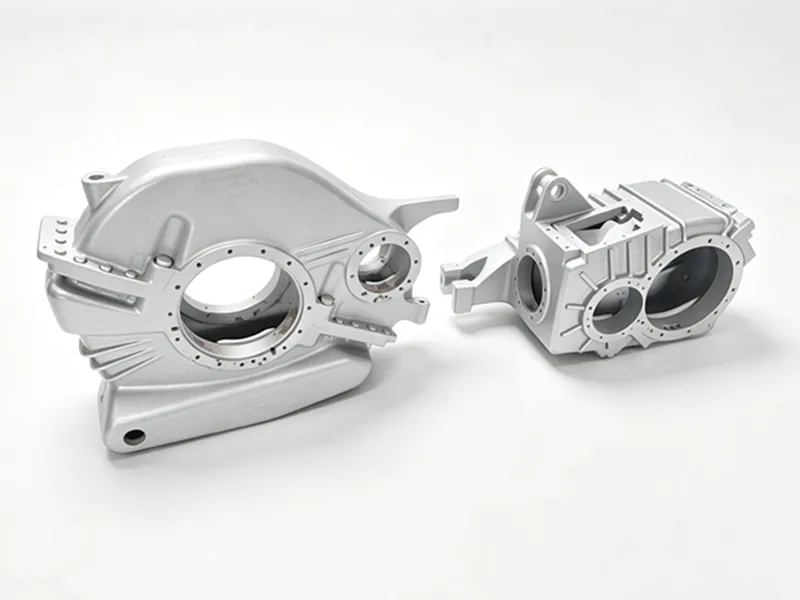
Cast aluminum alloy gearbox housings are an important application of aluminum in rail vehicle drivetrain systems. Casting allows complex housing geometries to be produced with integrated features for mounting, reinforcement, and internal component arrangement.
Al-Si-Mg casting alloys are relevant to this application. Research on aluminum alloys used for high-speed train gearbox housings has examined materials such as AlSi7Mg0.3 and the effects of casting defects on fatigue performance.
4.1 Casting and Subsequent Processing
Gearbox housings are produced by casting aluminum alloy into the required shape. Depending on the selected alloy and technical requirements, heat treatment may be applied to obtain the required mechanical properties.
Machining is then used to produce precise mounting surfaces, bearing seats, bolt holes, and other functional features. Dimensional accuracy is essential because these features affect component assembly and the alignment of drivetrain parts.
4.2 Casting Defects and Fatigue Performance
Casting quality has a direct influence on the reliability of gearbox housings. Porosity and other casting defects can act as stress concentration points, particularly when the component is subjected to repeated mechanical loading.
Research into high-speed train gearbox housings has investigated the relationship between pore size and high-cycle fatigue performance. This makes casting quality, defect control, and appropriate inspection important considerations in gearbox housing manufacturing.
The housing design, casting process, subsequent machining, and quality control work together to determine the performance of the finished component.

5. How Material Form and Processing Affect Train Manufacturing
The application of aluminum alloys in rail vehicles depends not only on the alloy grade but also on the material form and the processing route used to produce each component. The following examples illustrate how material selection and manufacturing processes work together in practical applications.
5.1 6005A Hollow Extrusions for Carbody Structures
For a carbody side wall or roof structure, 6005A aluminum alloy can be supplied in the form of large hollow extruded profiles. The extrusion cross-section can incorporate cavities and reinforcing ribs, allowing the profile to provide structural functions while limiting unnecessary material weight.
The profiles are cut to the required dimensions, followed by machining where necessary. Multiple profiles are then assembled and joined, with friction stir welding being one of the processes used in rail vehicle construction.
This manufacturing route integrates material selection, cross-sectional design, and welding into a coordinated structural solution. The final performance depends on the profile geometry, joint design, welding quality, and structural verification.
5.2 3003 and 5052 Aluminum Sheets for Interior Panels
Interior panels follow a different manufacturing route. Aluminum sheets are cut to size, punched where openings are required, and bent into the specified shapes.
3003 aluminum sheet is suitable for panels requiring good formability. 5052 aluminum sheet can be selected for components requiring greater strength while retaining good formability and corrosion resistance.
After forming, the components may undergo surface finishing to achieve the required appearance and service performance. The choice of alloy, sheet thickness, forming process, and surface treatment affects both manufacturing efficiency and the quality of the finished interior.
5.3 Cast Al-Si-Mg Aluminum Alloy for Gearbox Housings
A gearbox housing requires a more complex shape than a typical sheet component. An Al-Si-Mg casting alloy can be cast into a housing with integrated structural features and mounting sections.
After casting, appropriate heat treatment may be used where required by the alloy specification and component design. Machining then produces the precise interfaces needed for assembly, including mounting surfaces and bearing-related features.
Because casting defects can affect fatigue performance, the manufacturing process also needs to address casting quality and inspection. The combination of casting, any required heat treatment, machining, and quality verification determines the suitability of the finished housing for its service conditions.
5.4 Summary of Materials and Manufacturing Processes
| Component | Typical Aluminum Material | Main Manufacturing Processes | Key Considerations |
|---|---|---|---|
| Carbody side walls, roof, and floor structures | 6005A hollow extrusions | Extrusion, cutting, machining, and welding | Cross-sectional design, joint quality, structural strength, and fatigue performance |
| Selected structural components | 6082 extrusions or plates | Cutting, machining, forming, and joining | Required strength and component geometry |
| Interior panels | 3003 or 5052 aluminum sheet | Cutting, punching, bending, and surface finishing | Formability, surface quality, and applicable fire requirements |
| Gearbox housings | Al-Si-Mg casting alloys | Casting, applicable heat treatment, machining, and inspection | Casting quality, dimensional accuracy, and fatigue performance |
6. Conclusion
Aluminum alloys play an important role in modern rail vehicle manufacturing, particularly in carbody structures, interior components, and cast gearbox housings.
For carbody construction, 6005A large hollow extrusions offer an effective way to integrate structural functions into lightweight profiles, while welding processes such as friction stir welding support the assembly of these structures. For train interiors, 3003 and 5052 aluminum sheets provide material options for formed panels and related components. For gearbox housings, Al-Si-Mg casting alloys allow complex geometries to be manufactured, followed by machining to achieve the required precision.
Selecting the appropriate alloy, material form, and manufacturing process for each component is essential to achieving the required balance of weight, structural performance, manufacturability, and service reliability.
References
“Structural Design of Aluminum Hollow Extrusions for High-Speed Trains via Friction Stir Welding.” Metals, 2026, 16(5), 516. https://doi.org/10.3390/met16050516
“Correlation between Microstructures and Mechanical Properties of High-Speed Friction Stir Welded Aluminum Hollow Extrusions Subjected to Axial Forces.” Journal of Materials Science & Technology, 2018, 34(1): 102–111. https://doi.org/10.1016/j.jmst.2017.11.015
“Application of Friction Stir Welding to Construction of Railway Vehicles.” JSME International Journal Series C, 2004, 47(3): 502–511. https://doi.org/10.1299/jsmec.47.502
“Application of Friction Stir Welding to a Railway Car Body Made of Aluminium Hollow Extrusions.” JSME, 2005.
“Relationship Between Microstructures and Microhardness in High-Speed Friction Stir Welding of AA6005A-T6 Aluminum Hollow Extrusions.” Acta Metallurgica Sinica (English Letters), 2020, 33: 115–126. https://doi.org/10.1007/s40195-019-00970-8
“Effect of Pore Size on the High Cycle Fatigue Property of Al-Si-Mg Alloy for High Speed Train Gearbox Housing.” Fatigue & Fracture of Engineering Materials & Structures, 2025, 48(5): 2046–2053. https://doi.org/10.1111/ffe.14581
“Fatigue Failure Analysis of High Speed Train Gearbox Housings.” Engineering Failure Analysis, 2017, 73: 57–71. https://doi.org/10.1016/j.engfailanal.2016.12.008
“Application of Friction Stir Welding to Railroad Carbody.” DENKI-SEIKO, 2007, 78(2): 141–147. https://doi.org/10.4262/denkiseiko.78.141
EN 45545-2:2020+A1:2023. Railway Applications — Fire Protection on Railway Vehicles — Part 2: Requirements for Fire Behaviour of Materials and Components.